SOLUTION · HMI
fastHMI (Human Machine Interface)
fastHMI is a monitoring system that acquires data from production equipment, inspection equipment and utilities directly through PLCs and equipment interfaces and supervises it in real time. History is stored in hs-RTDB, our in-house real-time database, so changes in analog values can be tracked as trends, and abnormal conditions trigger on-screen alarms and SMS notifications. Integrated with MES/POP, fastHMI sends work orders and operating conditions down to equipment and reports equipment status and production results back up.
Key benefits
- Real-time equipment visibility — the whole line and each machine on one screen
- Early detection of abnormal conditions — fault and deviation signals sent at once by on-screen alarm and SMS
- Trend-based root cause analysis — analog history of temperature, pressure, power and more shows where values changed
- Utility data acquisition — temperature, humidity, pressure and power consumption recorded alongside equipment data
- MES/POP integration — work orders and operating conditions down to equipment, status and results up to the MES
- Fast screen configuration — an in-house HMI shortens development when equipment is added or changed
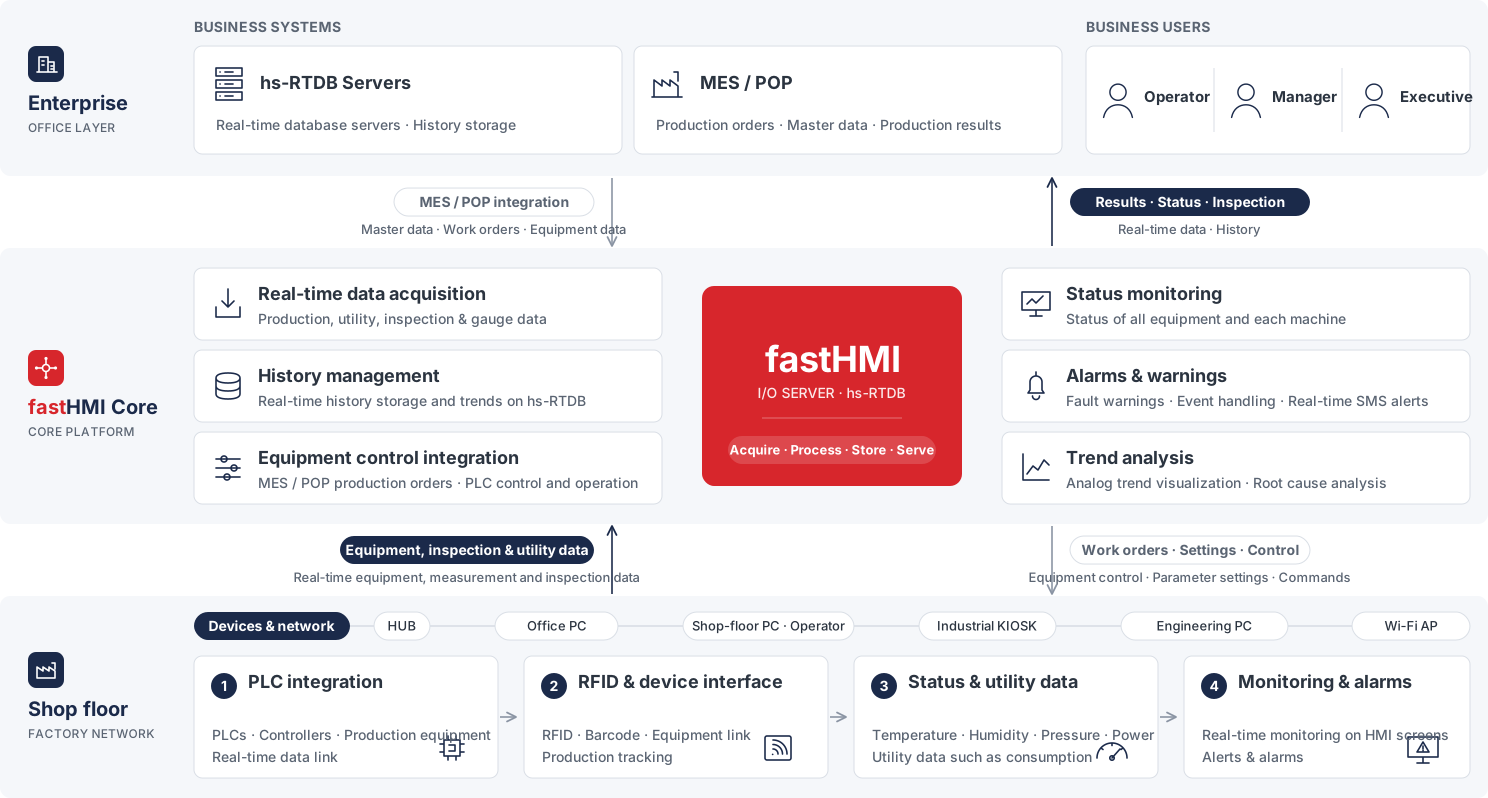
fastHMI integrated system architecture
A real-time monitoring platform that connects equipment data with operator interfaces
Data acquisition architecture
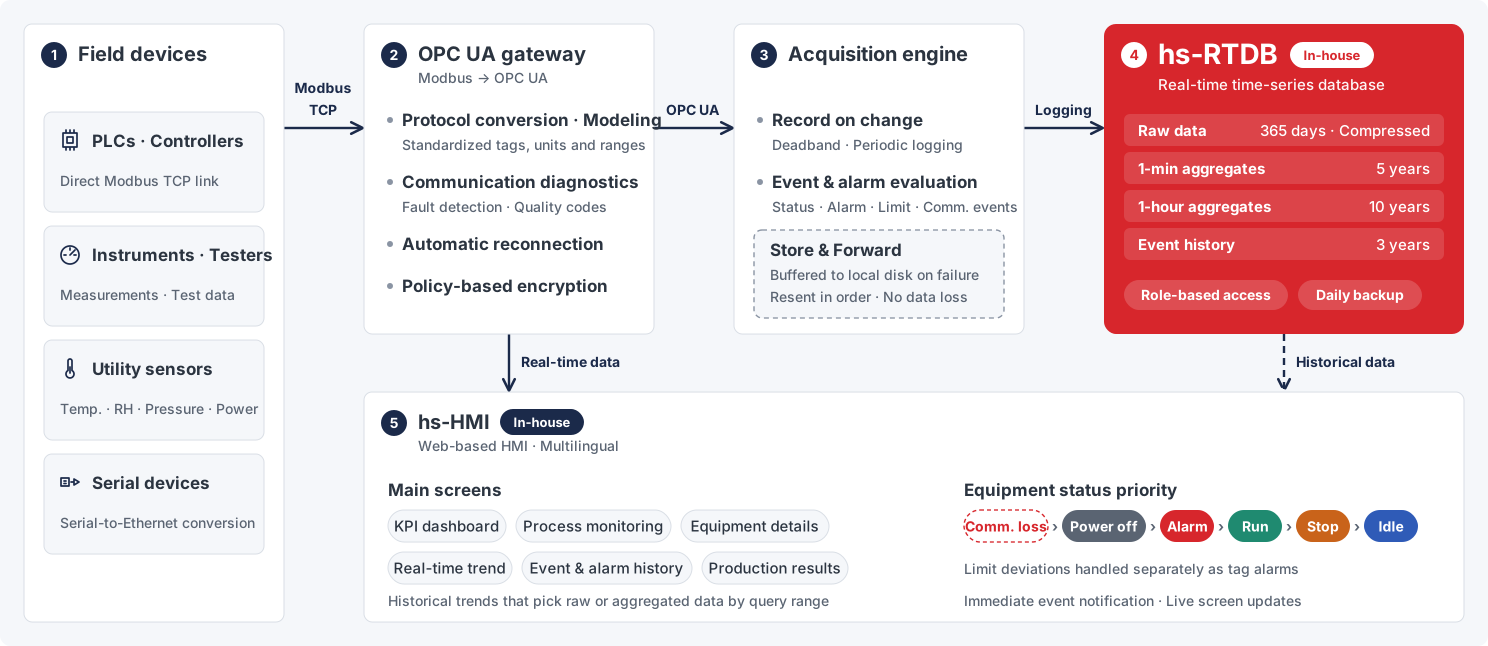
fastHMI acquires data from PLCs, measuring instruments and utility sensors in real time over Modbus TCP and OPC UA, and stores it as history in hs-RTDB, a time-series database developed in-house by Haesol. During acquisition it diagnoses communication status, evaluates events and alarms, and buffers data with store-and-forward to prevent data loss during network or database outages. Through hs-HMI, our in-house web HMI, users monitor equipment status, alarms and trends in real time and analyze historical data.
Hardware configuration
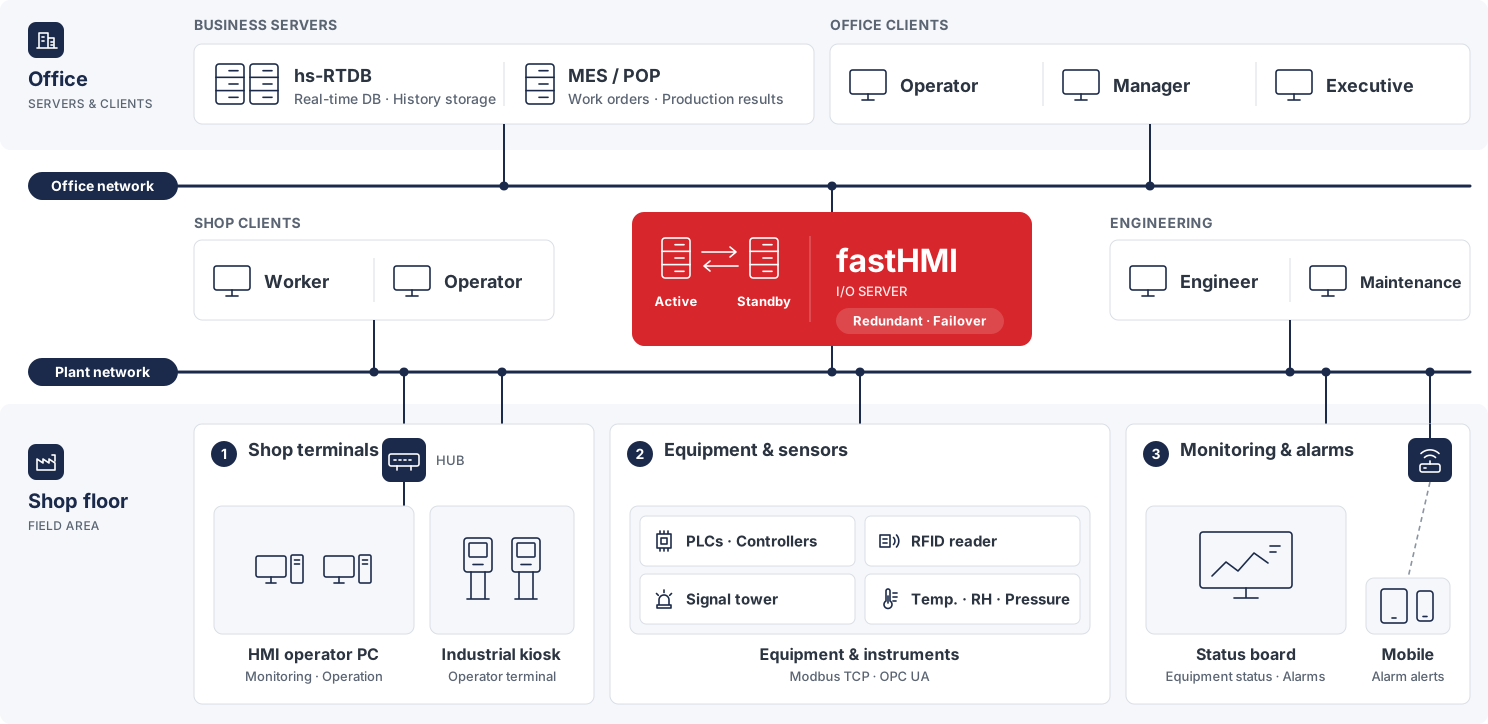
The hs-RTDB server and office PCs sit on the office network, with redundant fastHMI I/O servers between the office network and the plant network. Shop-floor PCs, kiosks, PLCs, sensors and status boards connect to the plant network over wired links, and mobile devices connect through wireless access points. (Solid line: wired · Dashed line: wireless)
Key features
Core functions for line-wide supervision, process monitoring, trends, alarms, equipment control and MES/POP integration.
Line 1RUN
42.5m/min 182℃
1,820 / 2,400
Line 2RUN
38.0m/min 176℃
2,210 / 2,400
Line 3ALARM
0.0m/min 214℃
960 / 2,000
Line 4RUN
45.1m/min 185℃
1,540 / 2,400
Line 5STOP
0.0m/min 24℃
0 / 1,600
Line 6RUN
40.2m/min 180℃
1,310 / 2,000
RUN 4ALARM 1STOP 1Today 61% complete
Integrated line monitoring
- Operating status and key process values such as speed and temperature by line
- Today's plan, production count, good lots and progress by line
- Stopped or abnormal lines identified at a glance by status color
Related modulesKPI dashboardProcess monitoring
- Output / plan72%
- Defects48EA
- Run time6h 12m
- Last downtimeCoil change
Line process monitoring
- Operating conditions by section: welder, reducing mill, annealer and cooling
- Plan, output and progress with good and defect quantities
- Run time, downtime and the last downtime reason
Related modulesProcess monitoringProduction results
Running 14Stopped 3Alarm 1C-03 · Oven temp. deviation
Equipment layout monitoring
- Equipment placed on layouts by floor and process area
- Running, stopped and alarm status of each machine by color
- Environmental data such as temperature and dew point by area
Related modulesProcess monitoringEquipment details
14:0014:1014:2014:30
- High temperature limit exceeded · H 75.0 ℃Unack
- Current fluctuation warningAck
Trends & alarms
- Historical trends of analog values such as speed, current and temperature
- Selectable time range, with a cursor to compare values at any point
- Operating status and alarm messages on equipment graphics
Related modulesReal-time trendEvent & alarm history
- Filling
- Conc. Inj.
- Mixing
- Transfer
Conc. SP 12.5 %PV 12.3 %Agitator 120 rpmTemp. 45.2 ℃
Batch process supervision & control
- Progress of batch steps such as filling, mixing and transfer
- Valve and pump states and tank levels
- Operating conditions such as concentration controlled by set point entry
Related modulesProcess monitoringEquipment details
Work order WO-0158LOT C2610290031Progress 1,240 / 2,000 m
Material inputDefect entryReport lot
MES/POP-integrated operation
- Dryer zone temperatures, supply fan speed and coating speed
- Work orders, material input, defect entry and lot reporting handled on screen
- Equipment operating data recorded together with production results
Related modulesProduction resultsProcess monitoring
Benefits
Equipment management built on floor rounds and handwritten operating logs moves to real-time, data-based supervision and analysis.
| Area | Before | After |
|---|---|---|
| Equipment supervision | Floor rounds, checking each machine's control panel separately | All lines and equipment supervised in real time on one screen |
| Response to abnormalities | Found and reported by operators, delaying action | On-screen alarm and SMS at once on a limit deviation or equipment stop |
| Operating records | Handwritten operating logs with gaps and irregular intervals | Process and utility data recorded automatically in hs-RTDB and kept long term |
| Root cause analysis | Causes guessed from incomplete records | Process values compared before and after an event using trends |
| MES integration | Work orders and results passed on by hand | Work orders and operating conditions sent to equipment, status and results reported automatically |
| Screen expansion | Long screen development whenever equipment is added | Screens configured and changed mainly by adding tags |